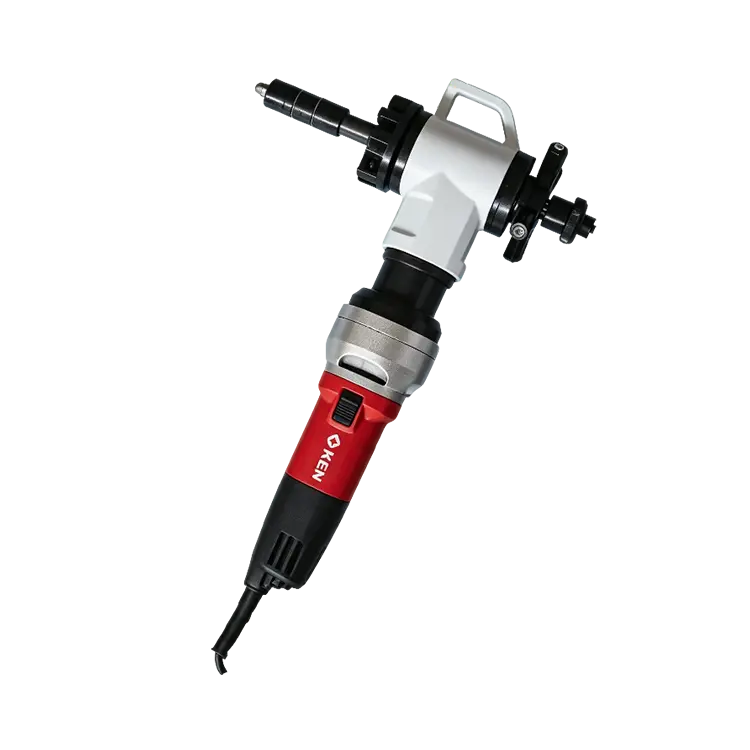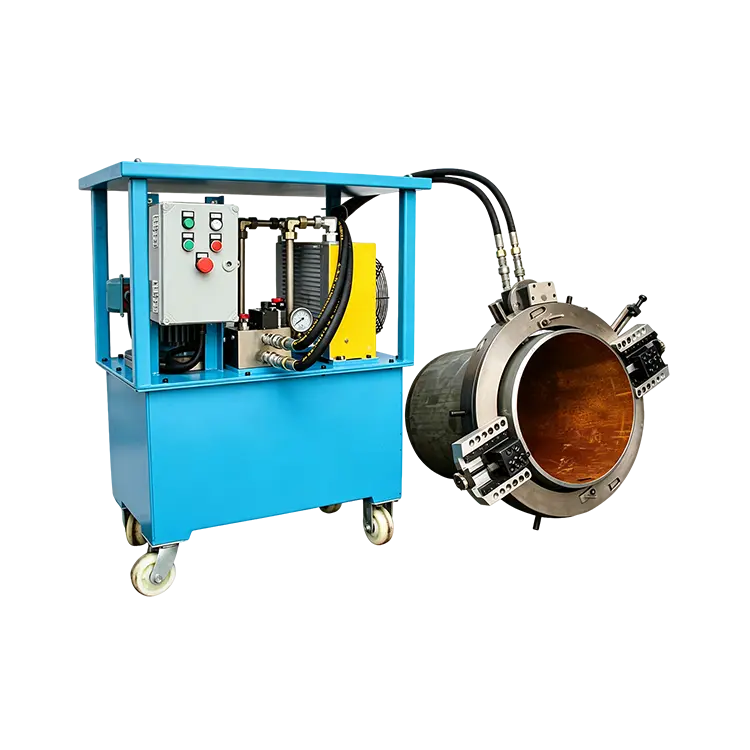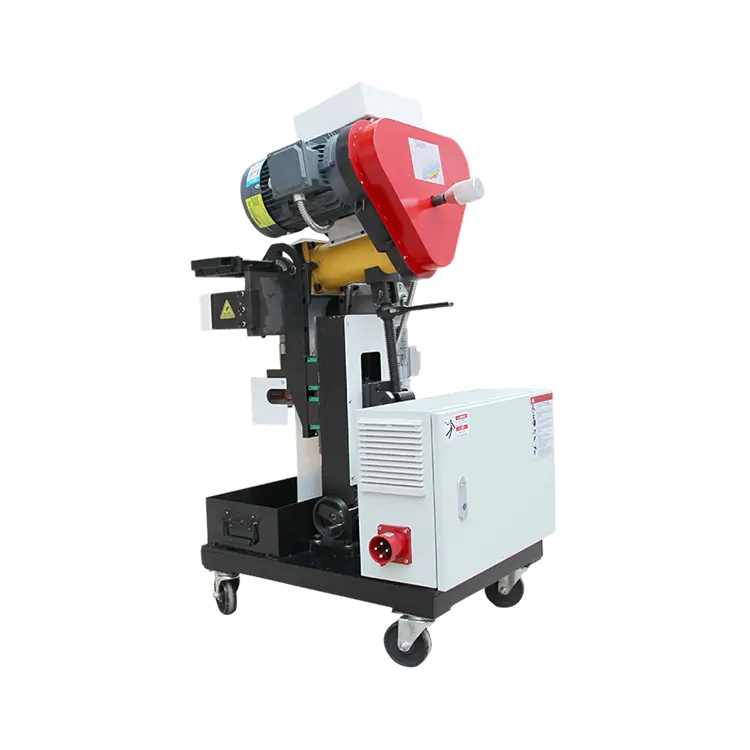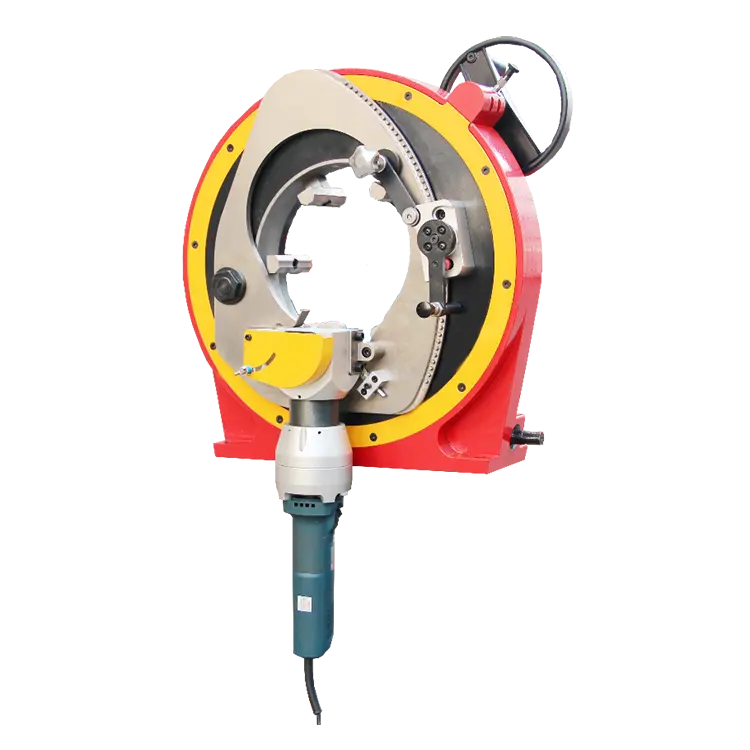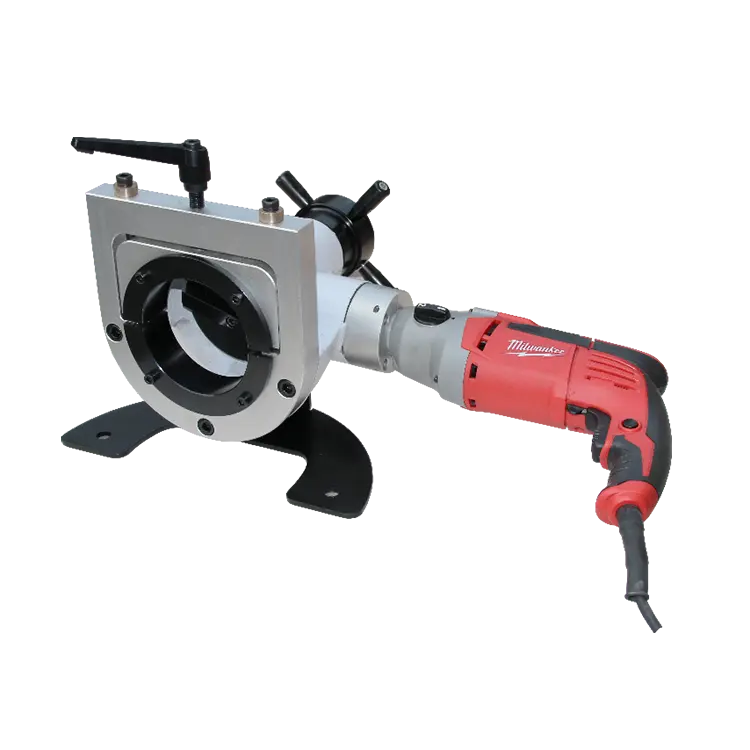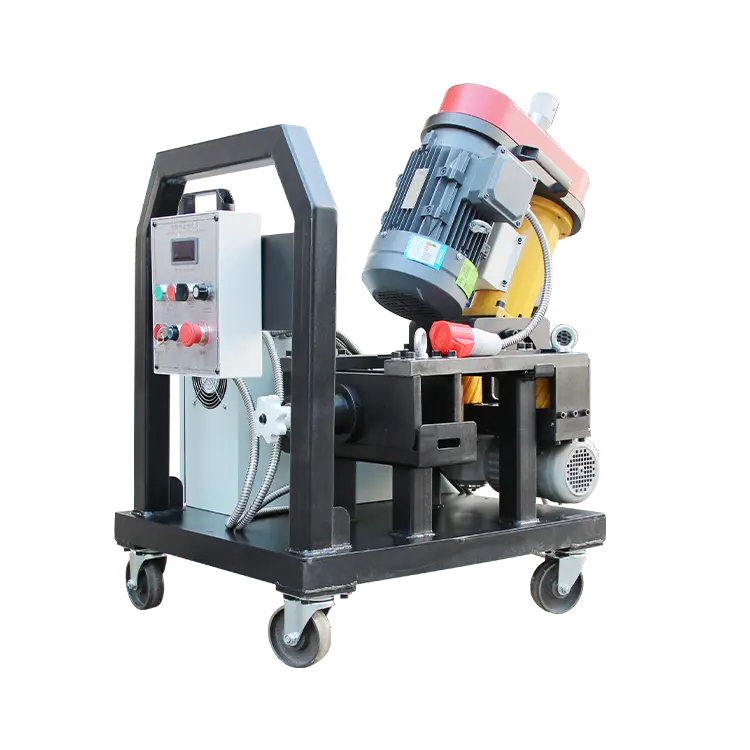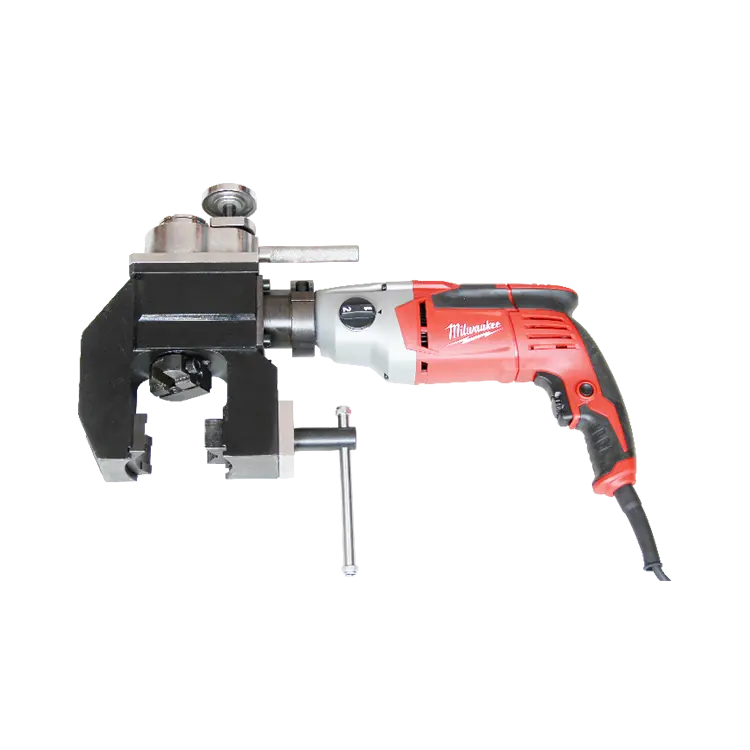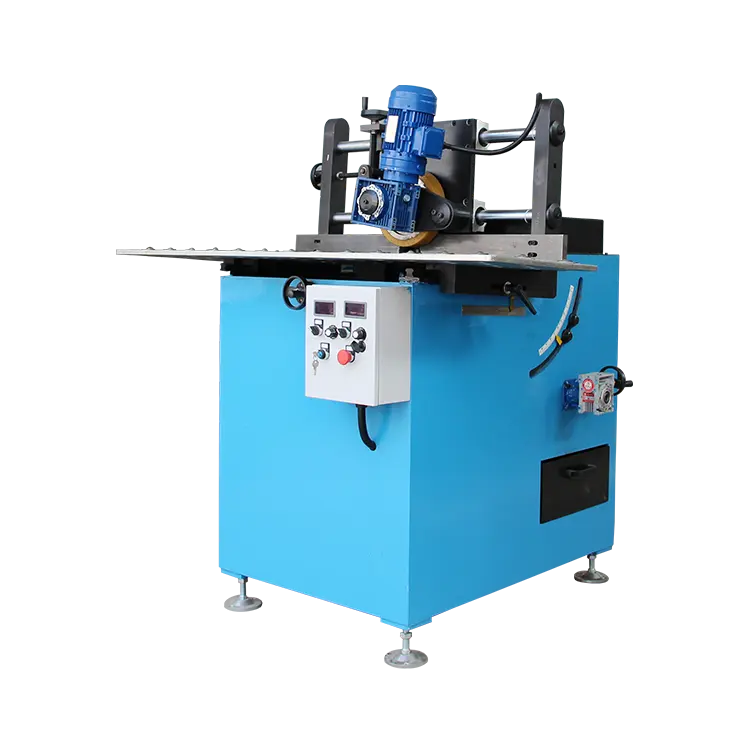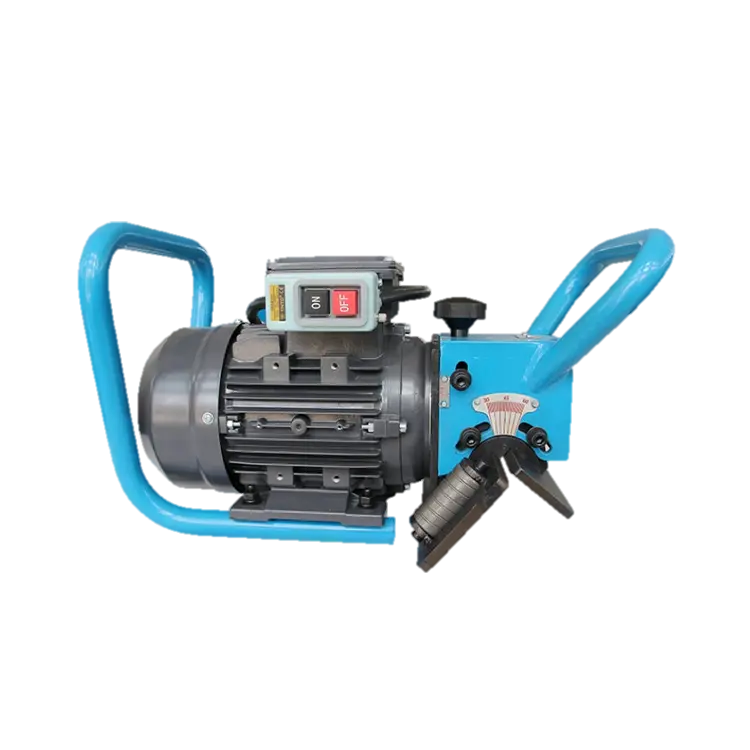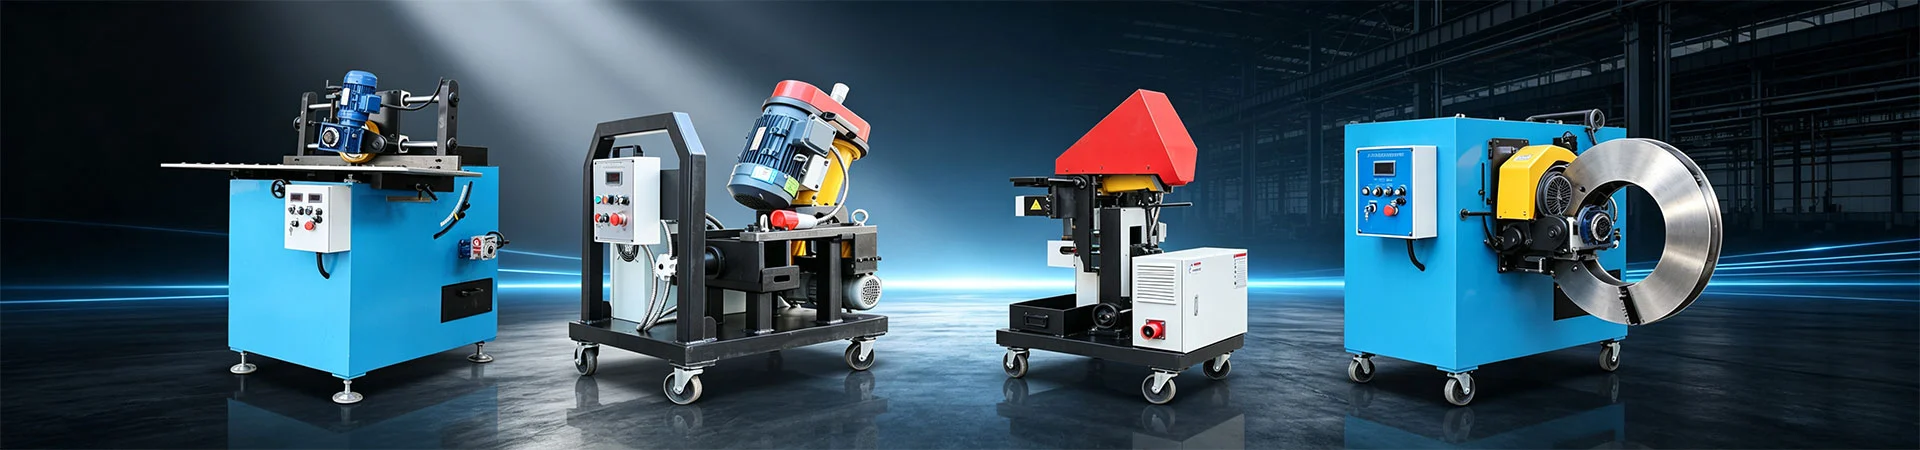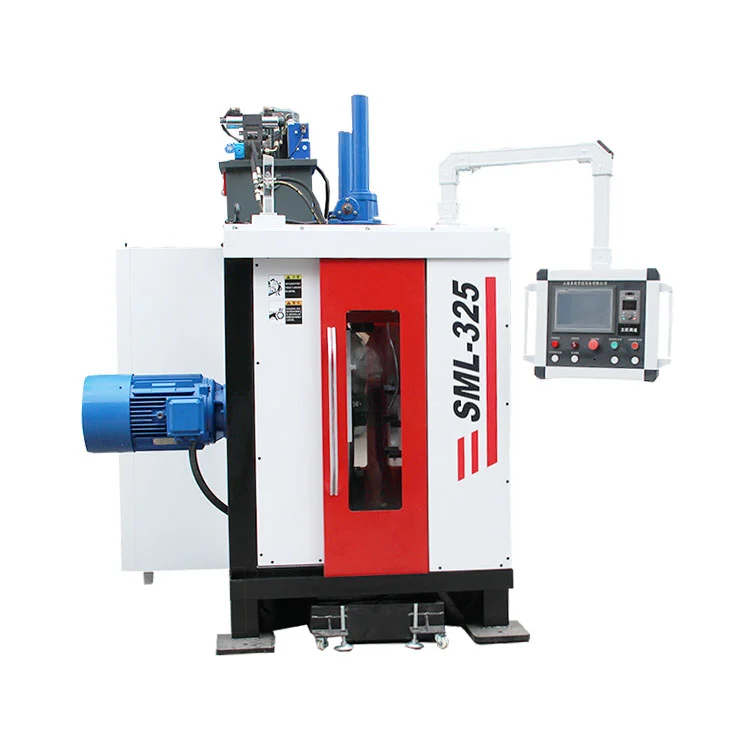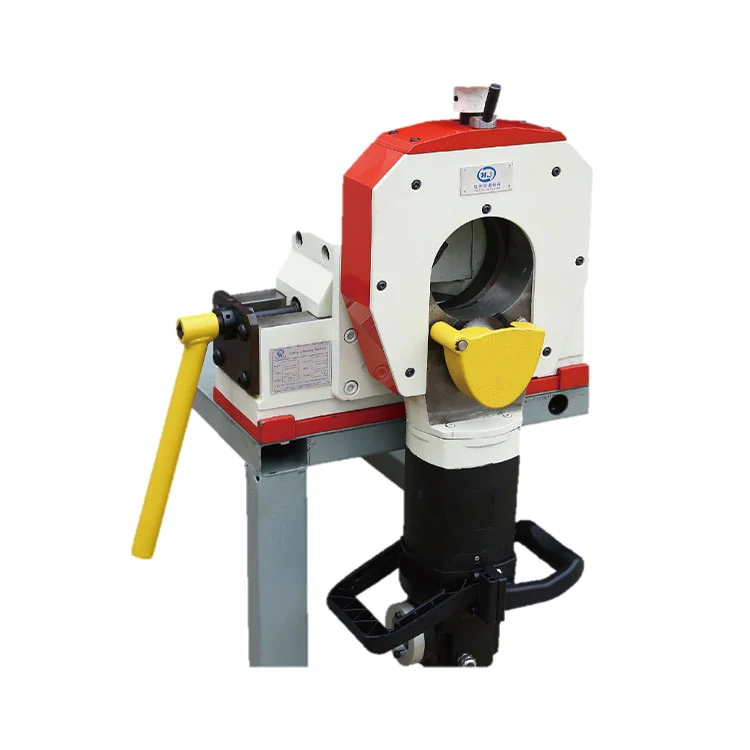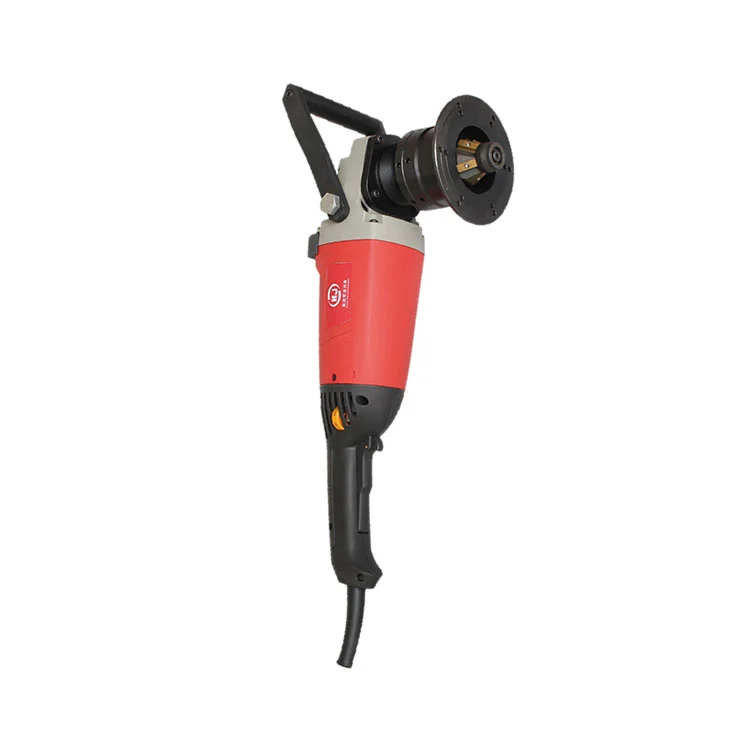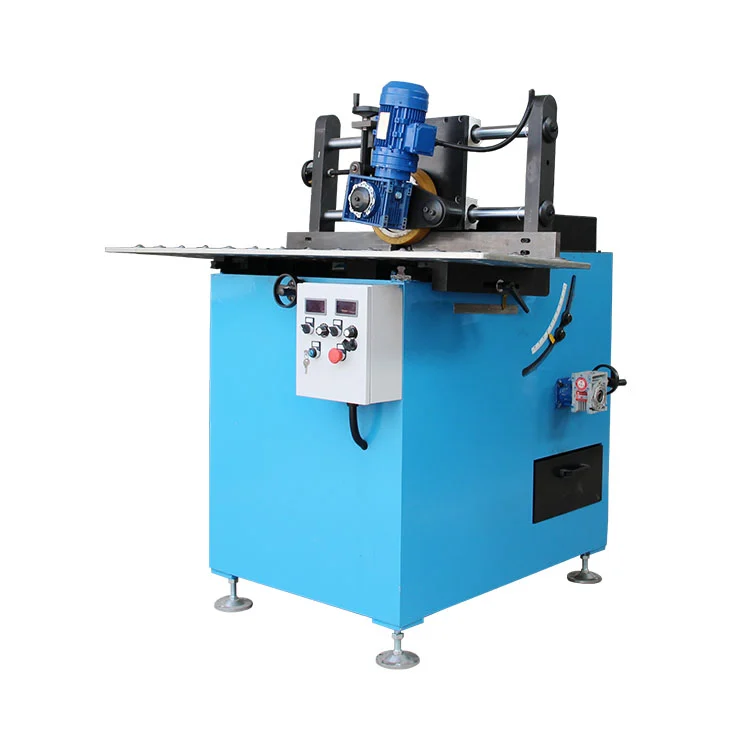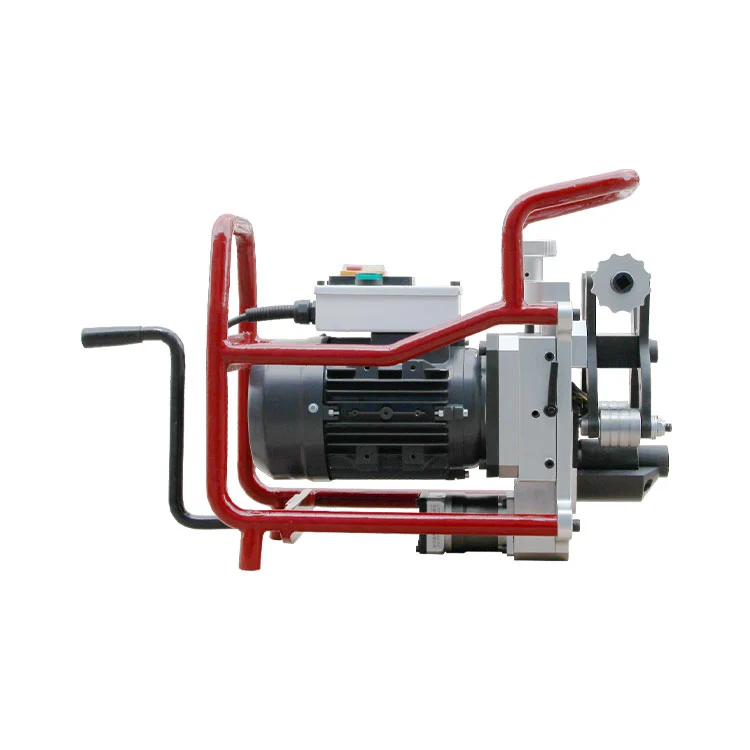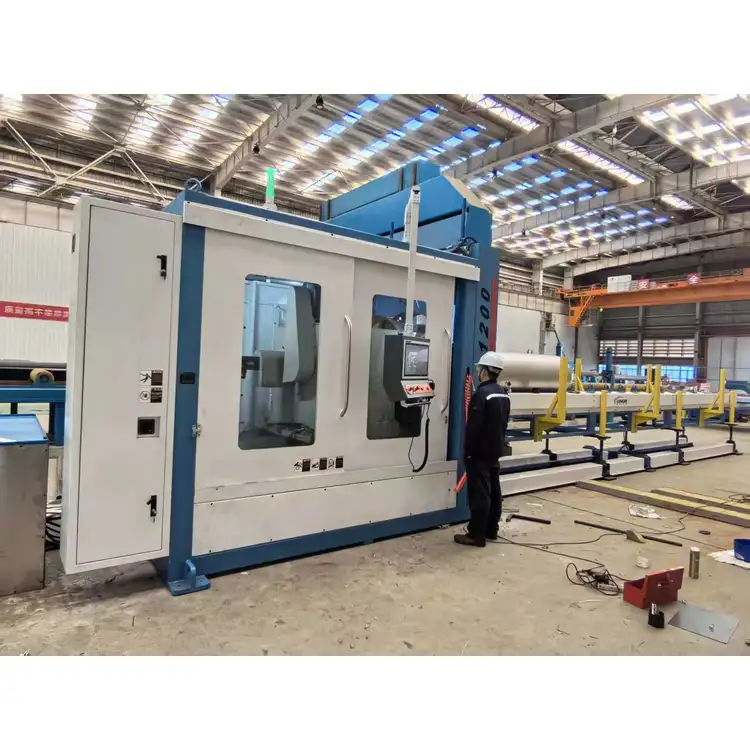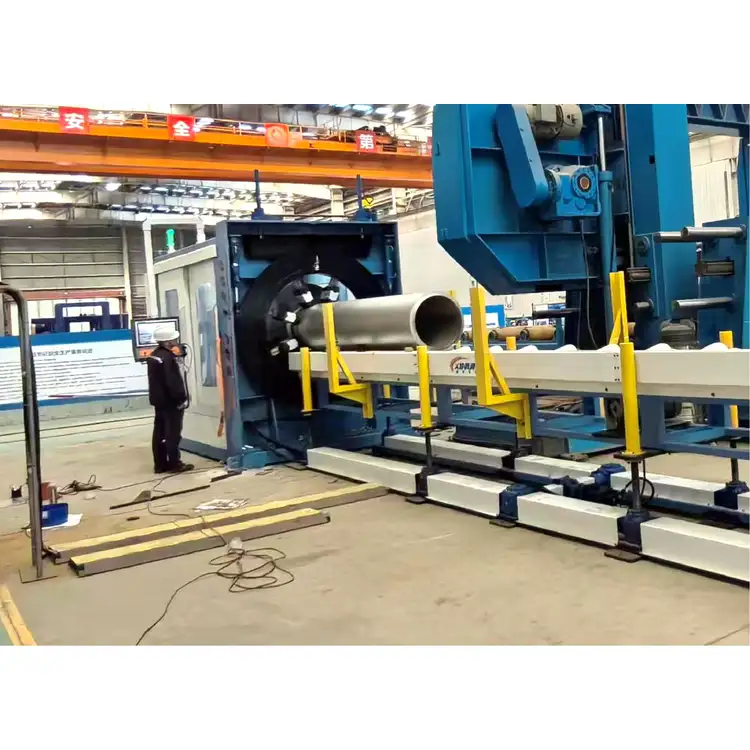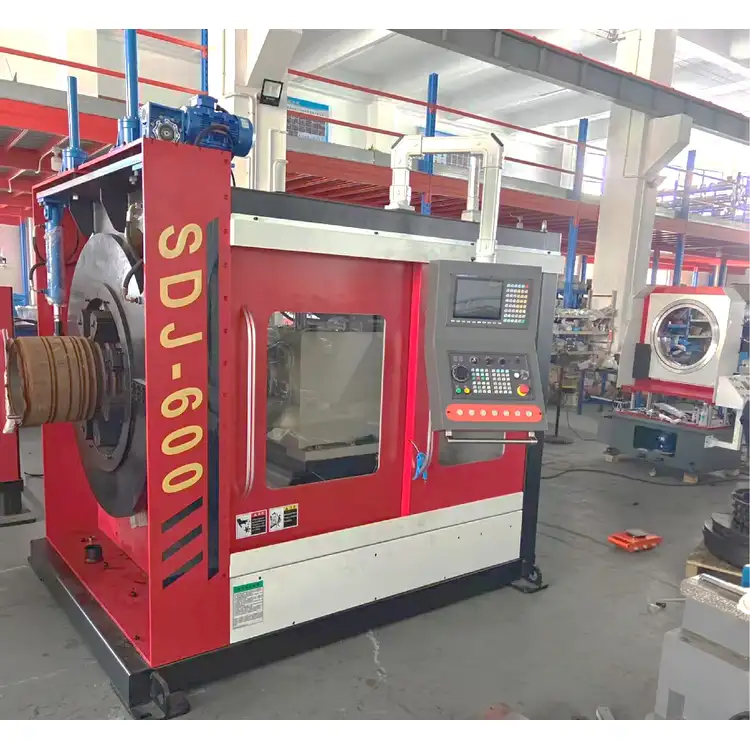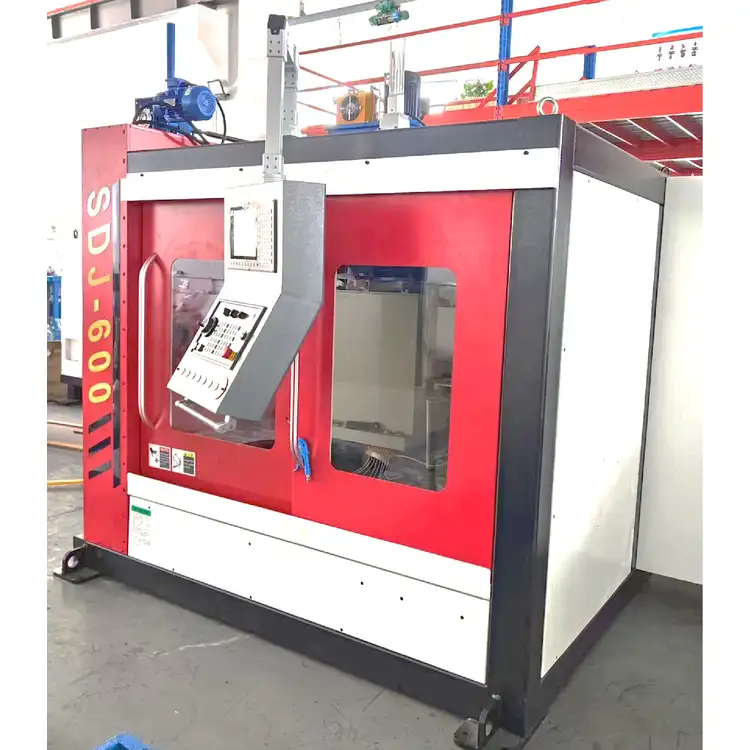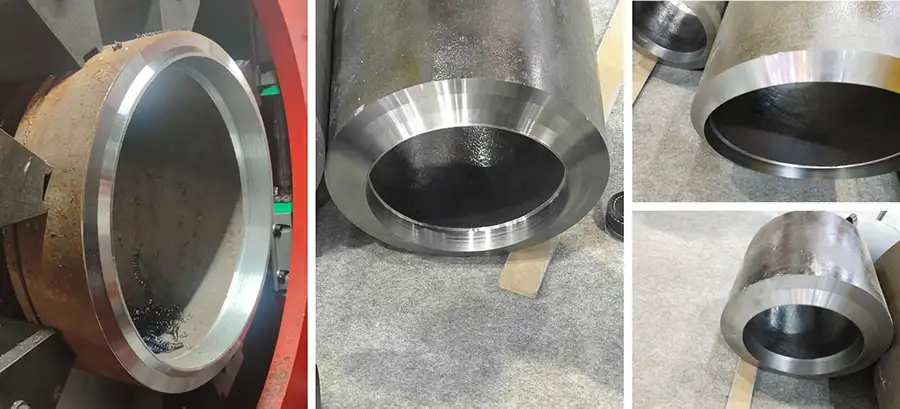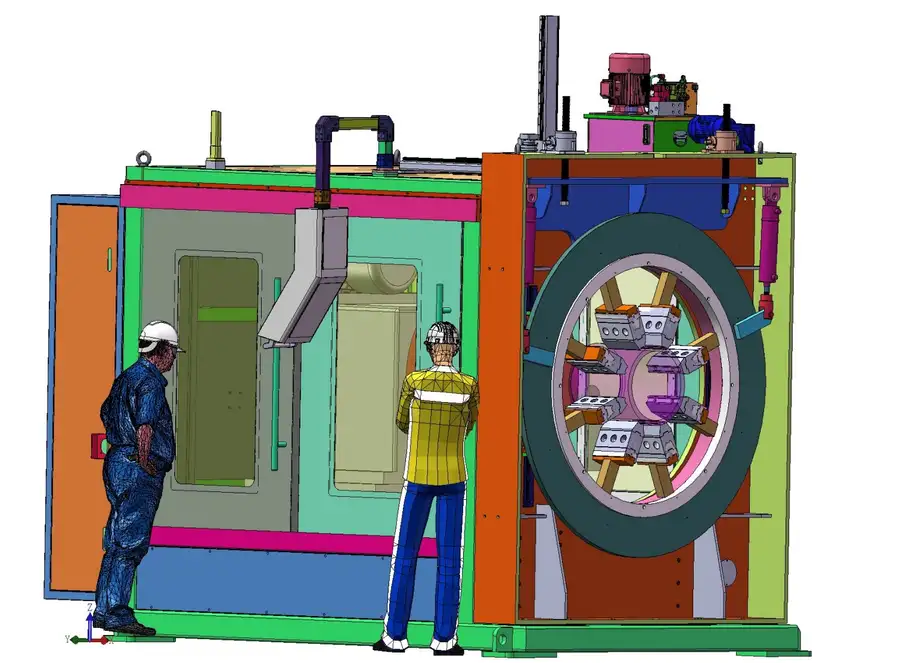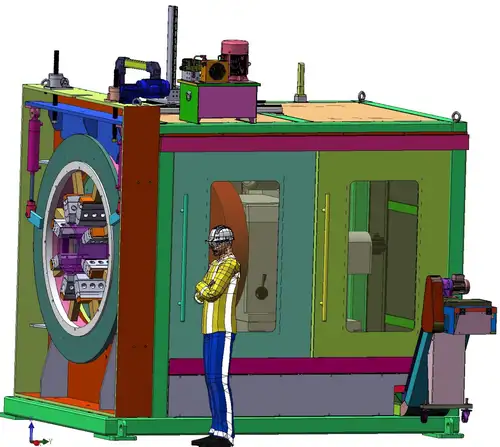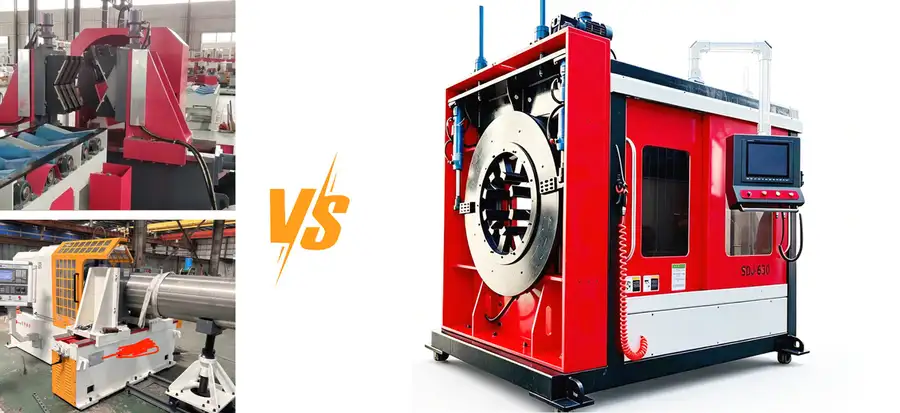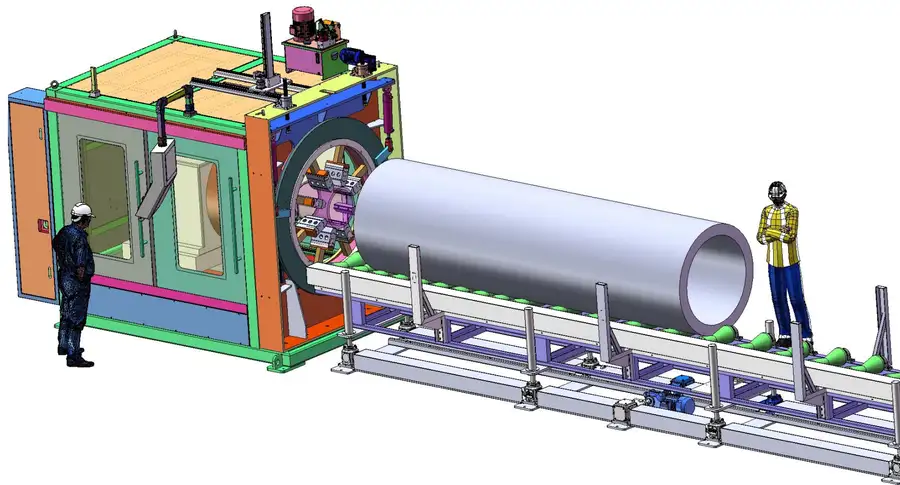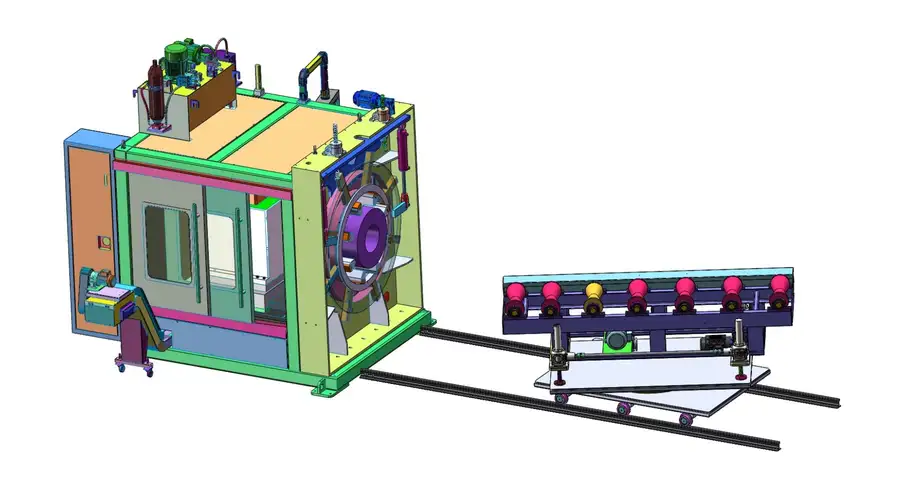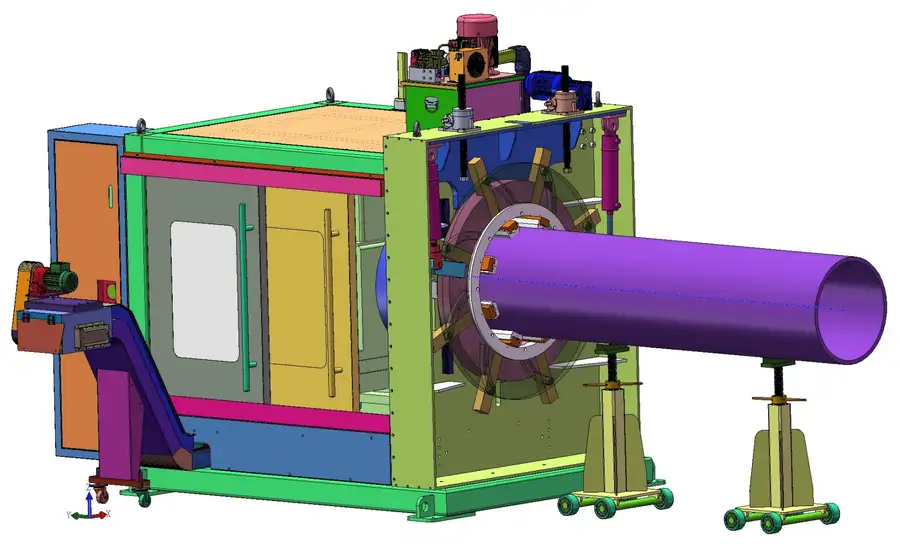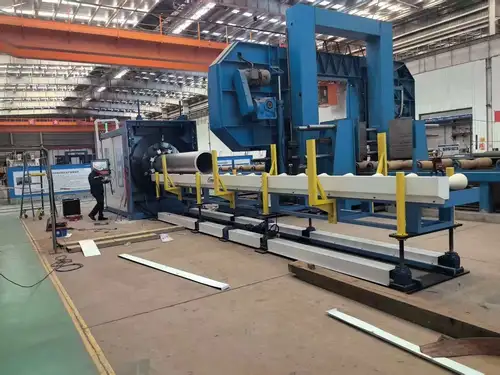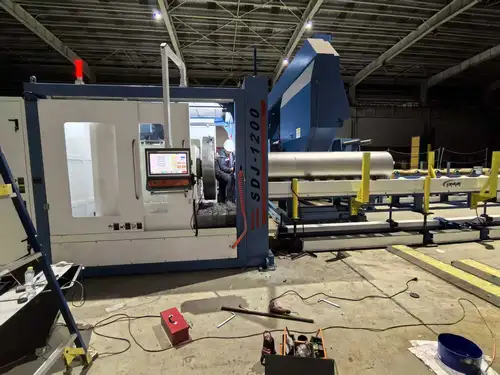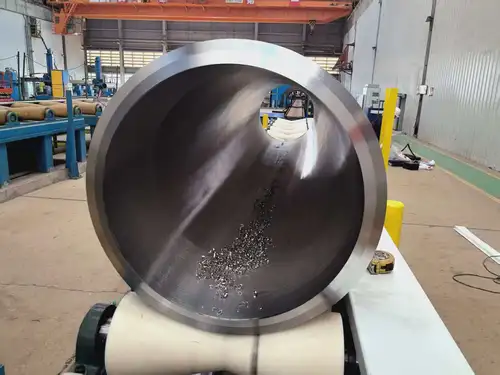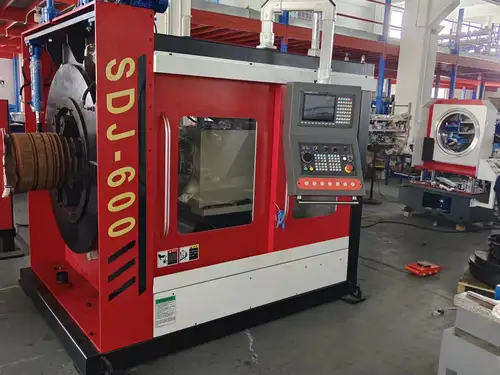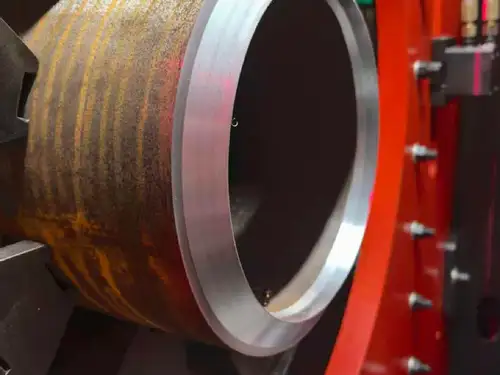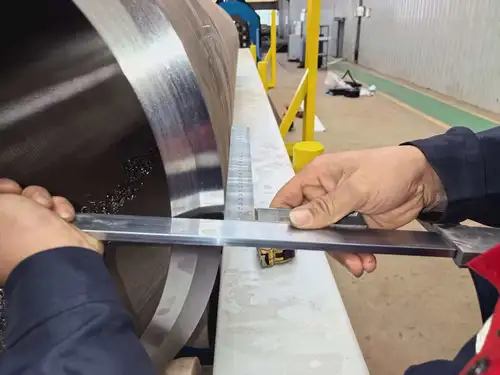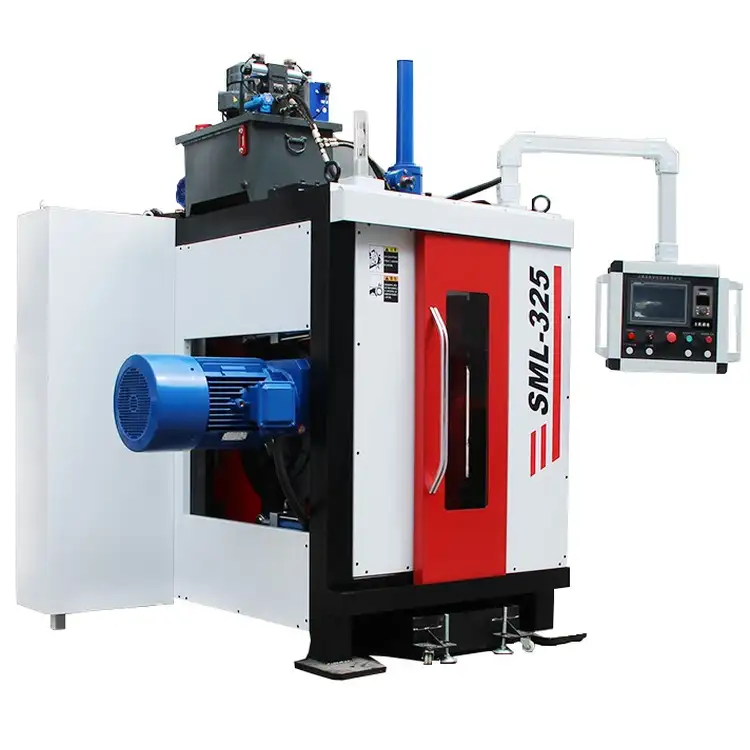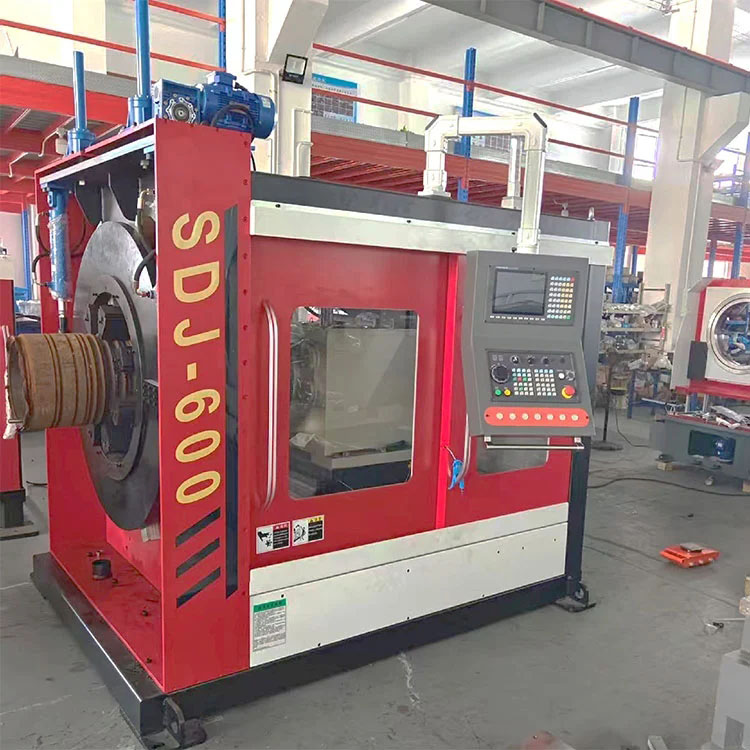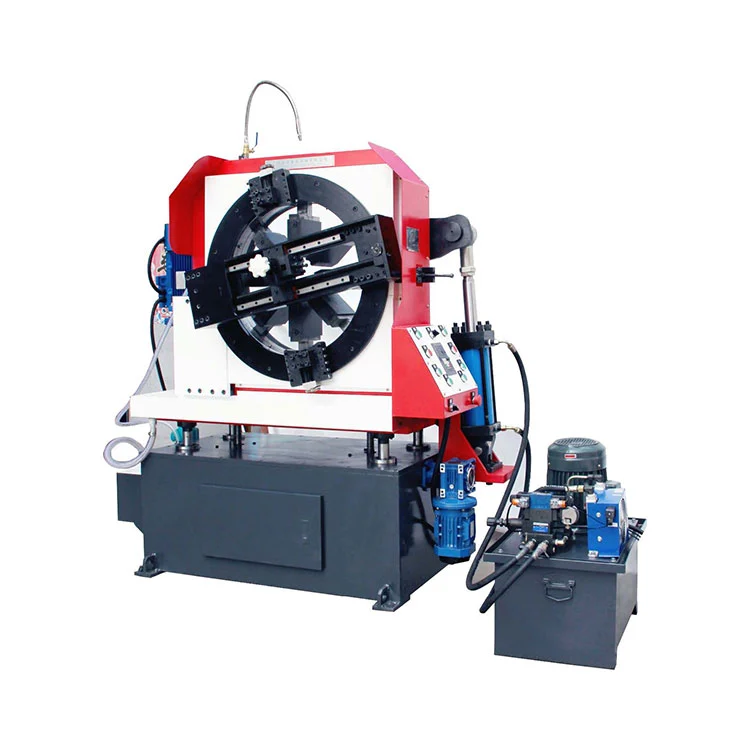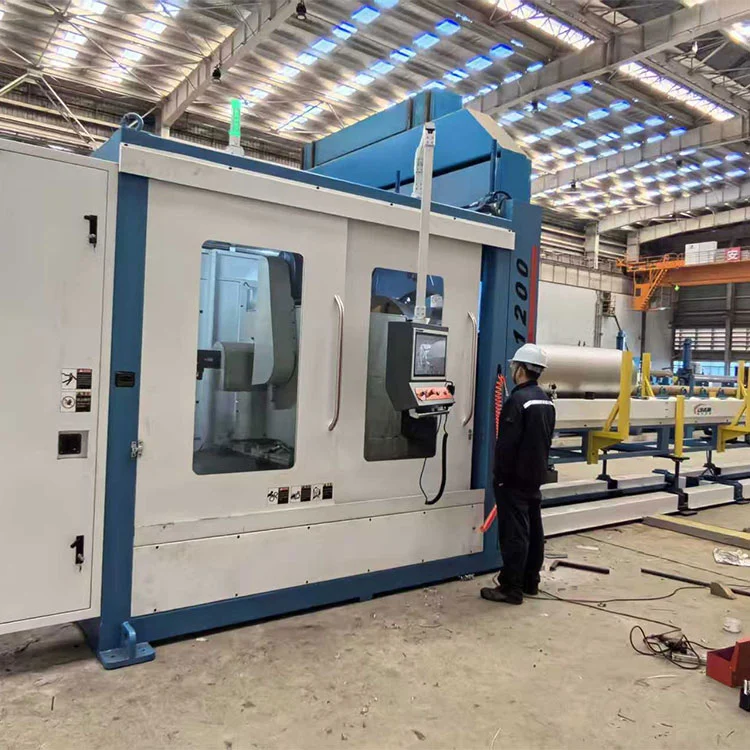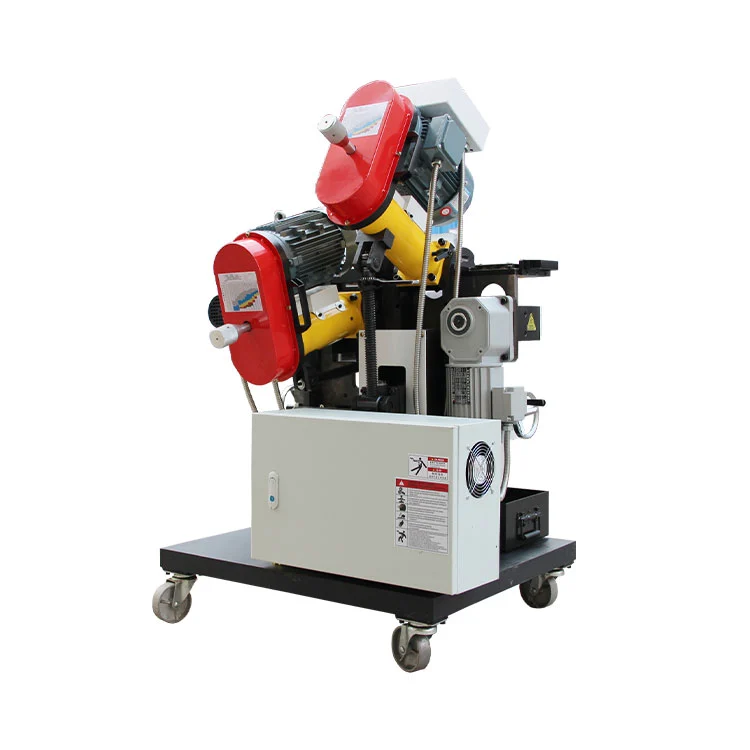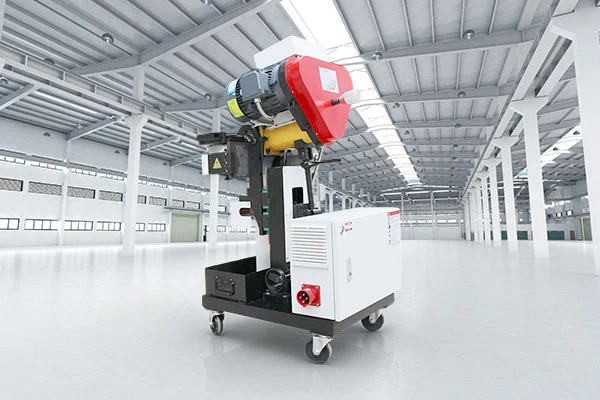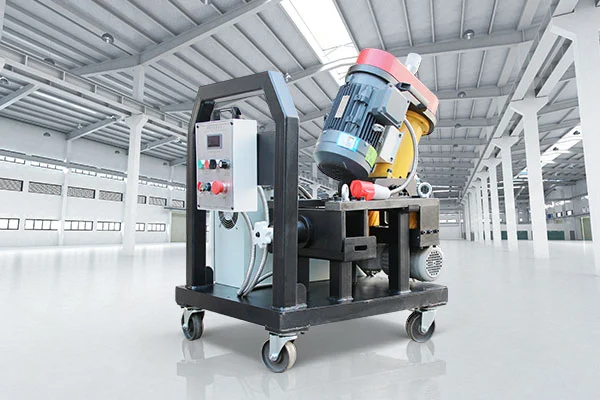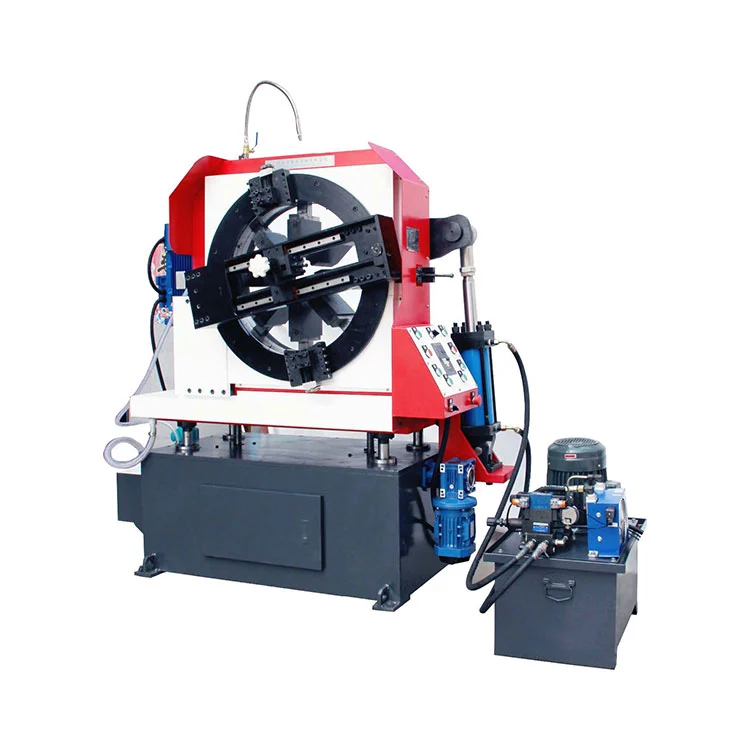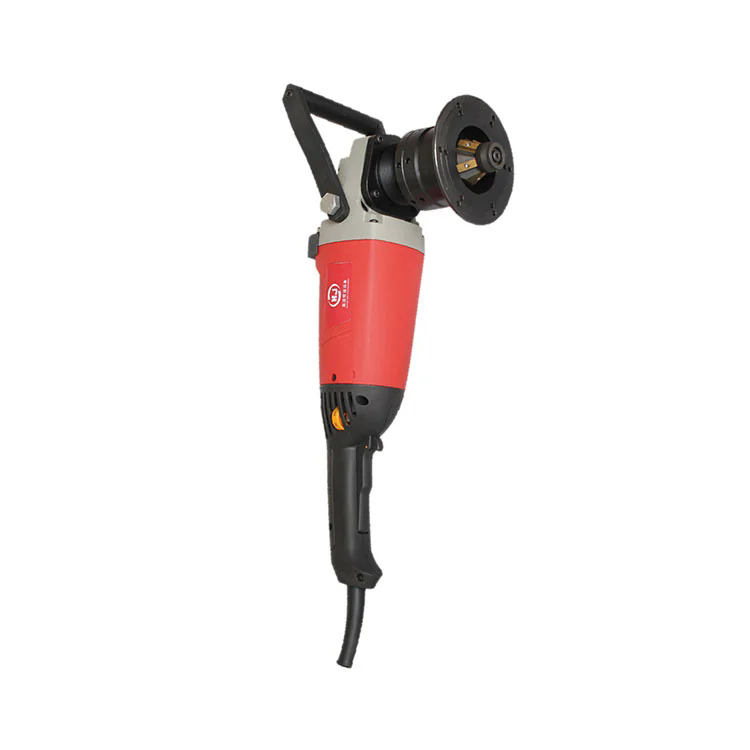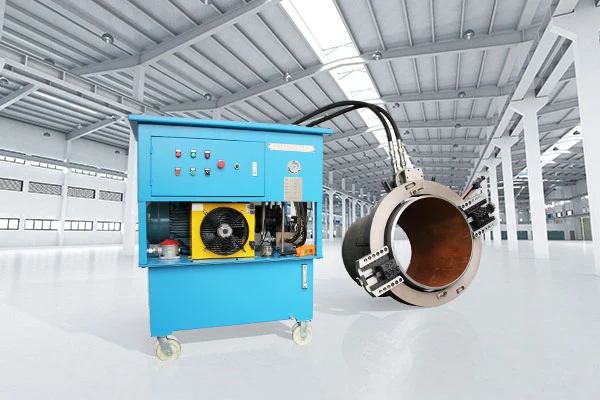
Centered on high precision, driven by high efficiency and distinguished by great flexibility, this CNC beveling machine pipe delivers outstanding performance to suit a wide range of application scenarios. The main unit features an integrally cast one-piece design. Leveraging the high precision of casting technology, it ensures accurate dimensions and uniform stress distribution across all sections of the machine frame. This provides a solid and reliable structural foundation for the stable operation of internal core components and guarantees consistent high-performance output of the equipment.
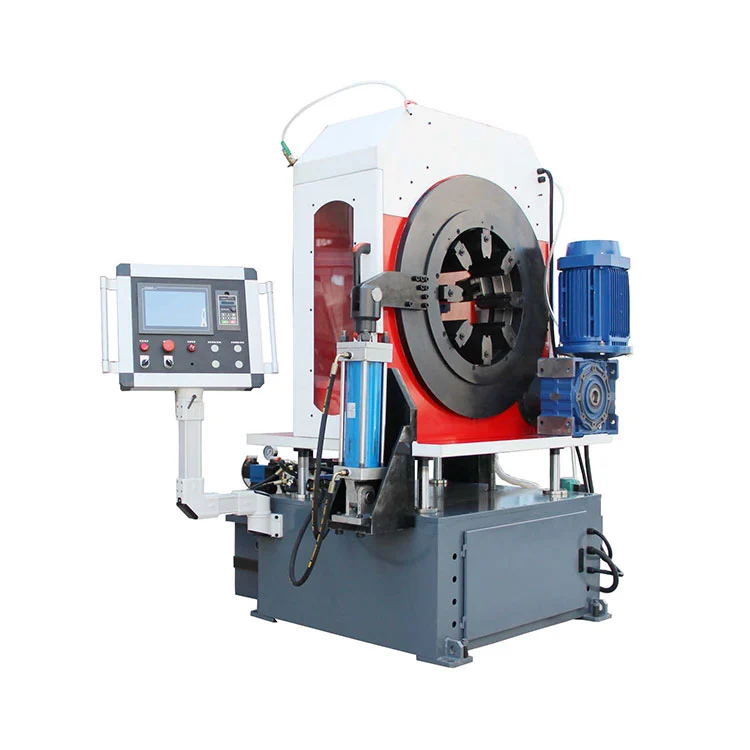
This CNC beveling machine pipe features a frame built from thickened material and precision-welded into a sturdy protective structure. It offers excellent impact and deformation resistance to fully shield core components. The base is fabricated from premium stainless steel with superior corrosion and wear resistance for a longer service life, boasting a smooth, refined and attractive appearance.
The main body adopts an integrally cast one-piece design. Benefiting from high-precision casting, it ensures precise dimensional control and even stress distribution throughout the frame. This creates a robust structural base for stable operation of internal core parts and sustains consistent high-performance output.
An 8-jaw clamping configuration is customized for pipe gripping. Compared with conventional clamping methods, the 8-jaw design enlarges contact area with the pipe and reduces pressure per unit area. It achieves firm clamping and stable machining while protecting pipe profile and surface from deformation and damage.
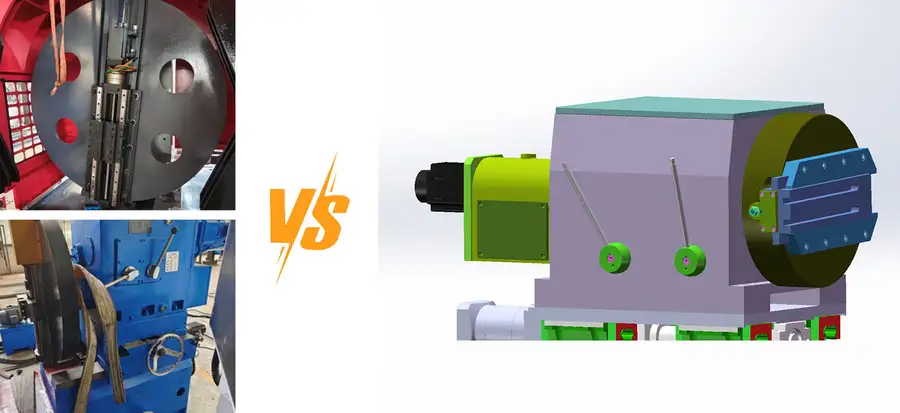
The feeding system is driven by a rear-mounted motor, replacing the traditional front motor plus slip ring transmission setup. This improvement eliminates common high-failure issues such as poor contact, wear and aging associated with front motor and slip ring assemblies. It enhances stability and reliability of the feeding drive and cuts downtime for maintenance.
Equipped with dual linkage for vertical lifting and horizontal movement, the mechanism completes pipe position calibration automatically without repeated manual adjustment. It streamlines centering procedures, delivers accurate pipe alignment, reduces labor intensity and boosts working efficiency.
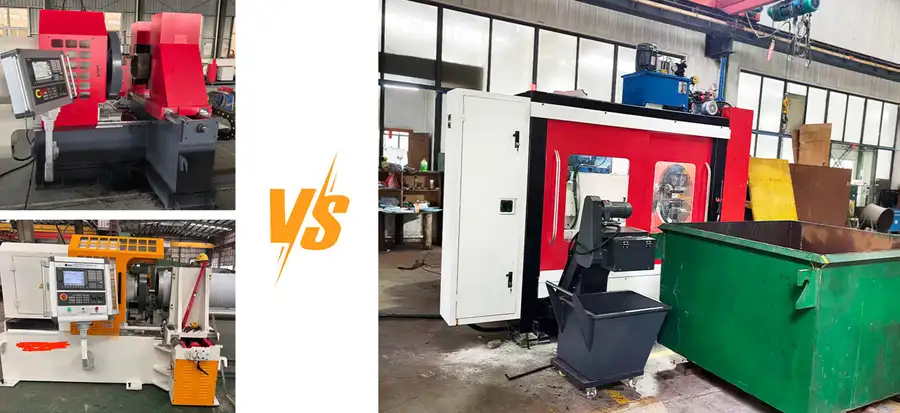
The independent rear chip removal module is separated from the core machining zone. This layout prevents chips from interfering with machining accuracy, facilitates residue cleaning and component servicing, lowers routine maintenance difficulty and improves overall equipment maintainability.
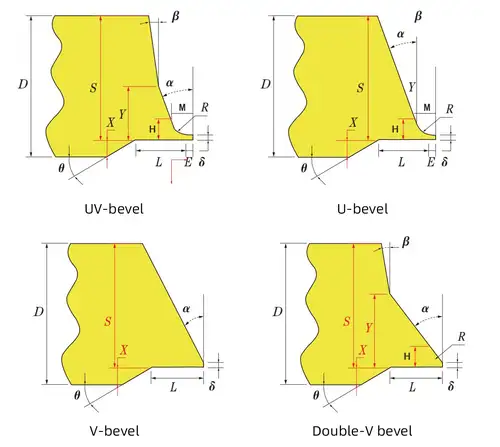
Other bevel profiles can be customized as required.
High-definition LCD display
Simply set parameters; variable data can be collected and stored in system memory or SD card. Data can also be saved, analyzed and verified via Ethernet or USB.
Controlled by EtherCAT or MIII bus for better real-time performance and easier maintenance.
Built-in IoT interface to access machining data in real time for simplified management.
Supports expandable application software modules. Required modules can be added as plug-ins according to customer requirements.
2 GB RAM paired with 8 GB storage delivers outstanding execution speed.
Centered on high precision, driven by high efficiency and distinguished by great flexibility, it delivers superior performance to accommodate diverse application scenarios.
Input Interface: Receives signals from external devices, including keypad inputs on the machine operation panel, signals from various sensors (position sensors, temperature sensors, etc.), and NC machining programs transmitted by external equipment. Common input interfaces include USB, serial port and Ethernet for easy connection and data exchange with different peripherals.
Output Interface: Transmits control signals processed by the CNC system to machine actuators such as drive motors, solenoid valves and indicator lights to govern machine motion, actions and status indication. The type and format of output signals shall match the connected actuators to guarantee accurate signal transmission and execution.
LCD or touchscreen is generally adopted to display the CNC operation interface, machining programs, process parameters, machine status, alarm messages and more for convenient monitoring and operation by operators.
Supports communication with external devices. It can exchange data with host computers to realize remote monitoring, program transfer and system upgrade, or network with other CNC equipment for coordinated operation and centralized management of multiple machines. Wired communication is available.
Adopting an advanced multi-core CPU architecture and powerful supercomputing-grade platform, it delivers an ultra-smooth operating experience.
Equipped with 2 GB memory for smooth program execution and reliable handling of diverse tasks.
High anti-interference design, passed 4.5KV EFT test and CE certification.
Supports highly stable RS485 communication for reliable expansion of peripheral devices.
Max. 256 I/O points available to control more mechanisms.
Supports up to 64-axis control for exceptional control capability.
USB 3.0 port enables fast and convenient program import and transfer.
Program block look-ahead reaches 8000 Blocks/s for superior processing performance.
RT-Linux embedded control system platform
Full-compilation execution module
Configurable IoT development platform
Remote assistance for fault diagnosis and system upgrade
Platform-based design concept
64-bit high-speed and high-precision contour control
Conversational assisted program editing
Special curve machining: Supports constant surface speed machining for parabolas and spline curves to achieve superior surface finish. The spline teach function automatically fits curves between points via cubic equations for smoother profiles compared with conventional teach modes.
Integrates open UI and PLC platforms. Customers can freely customize interfaces and functions to achieve highly personalized operation.
Self-definable permission allocation greatly enhances system flexibility and adaptability, allowing customized access rights for different users.
Supports graphic simulation, conversational programming and custom M-code functions.
Fast execution: Short PLC scan time enables rapid response to machining commands and improves productivity.
Automatically tracks workpiece position via vision and collects positional data in real time to facilitate industrial automation control.
Direct connection with smart cameras; PC-BASE mode is also available to realize vision positioning, flying shoot and other functions.
Connects up to 8 vision systems to realize graphic integration and data analysis from multiple cameras.
Supports servo tension control with PID adjustment and master ratio functions, which can be used in combination. Master ratio includes active nonlinear master ratio and feedback linear master ratio.
Dedicated control system, servo drives and UPS modules are available.
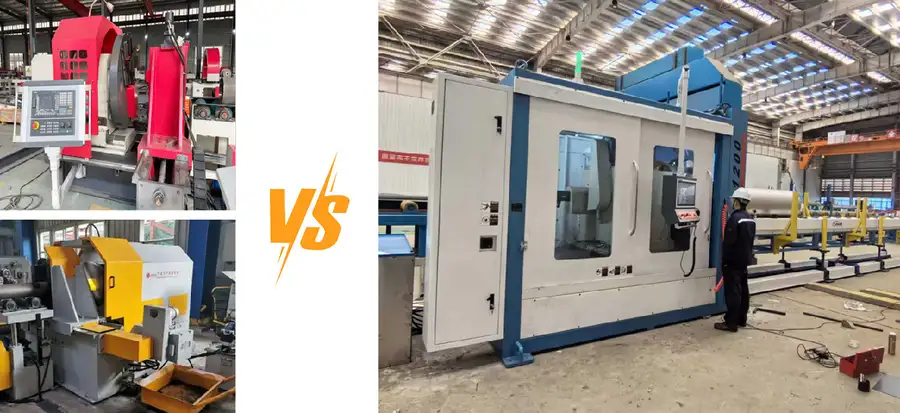
| Xianjin Pipeline | VS | Domestic peers |
| Self-centering multi-jaw clamping for high precision | Clamping Method | V-type clamping suffers poor repeat positioning accuracy and tends to deform thin-walled pipes |
| Rear servo motor for feeding & retracting; high machining efficiency (1–2× higher than domestic peers) and enhanced stability | Feeding Mechanism | Front-mounted motor: slow retracting speed and low efficiency; rear slip rings bring high failure rates |
| Hard-rail design for the tool post feeding mechanism, precision ±0.1 mm | Feeding Mechanism | Some manufacturers use linear guides with accuracy of 0.5–2 mm |
| Full machine guarding for improved safety | Safety Guarding | Partial front guarding: chips splash outwards |
| Gear shifting + spindle variable frequency speed control for greater torque | Spindle Housing | Spindle variable frequency speed control only, resulting in low torque during low-speed machining |
| 2.3 kW high-power feed motor, delivering twice the machining capacity of domestic peers | Feeding Mechanism | Low-power front-mounted motor with low rapid traverse speed |
| All gears inside the gearbox are ground | Spindle Housing | Some manufacturers adopt directly hobbed gears, causing loud noise |
| Integrally cast main body; hard rails adopted across the full range for excellent machine rigidity | Main Unit | Linear guides used on machines from some suppliers |
In summary, this CNC beveling machine pipe achieves 1–2 times higher overall efficiency and 5–10 times better machining accuracy than competing models. Its clamping range for wall thickness is better optimized for pipe machining.
Product Comparison – Overall Guarding
Product Comparison – Equipment Clamping
Product Comparison – Chip Removal System
Product Comparison – Feeding Mechanism
SDJ-400 Main Technical Parameters (Machining Range: Φ30 – Φ457)
| Number | Parameter | Remarks |
| Machining Range | Φ30- Φ 457 | |
| Machinable Wall Thickness | 3-100mm | |
| Bevel Profiles | V, Double V, U, UV, I and other bevel profiles | Custom additional bevel profiles available |
| Clamping Method | Hydraulic multi-jaw clamping | 8-jaw synchronous clamping |
| Control System | Yida, Taiwan | Other control systems optional |
| Suitable Workpiece Materials | Carbon steel, alloy steel, stainless steel, low-temperature steel, etc. | |
| Main Motor Power | 4KW | |
| Feeding Speed | Servo control | Adjustable |
| X-axis Servo Motor Power | 2.3KW | |
| Y-axis Servo Motor Power | 2.3KW | |
| Main Unit Guarding Type | Full frame guarding | |
| Chip Removal Type | Rear slat-chain chip removal system | Standard |
| Hydraulic Motor Power | 2.2/ 5 | Optional |
| Vertical & Horizontal Axis Locking Method | Manual / Automatic | Optional |
| Screen Size | 15-inch, 19-inch | Optional |
| Main Unit Lighting | Available | RED lighting |
| X-axis Repeat Positioning Accuracy | ±0.1 | |
| Y-axis Repeat Positioning Accuracy | ±0.1 | |
| Main Motor Transmission Type | Heavy-duty V-belt | |
| Boring Depth | ≤150mm | Standard tool shank: 100 |
| Spindle & Cutter Head Speed | 20–200 rpm | Stepless speed regulation, spindle VFD speed control |
| Tool Type | Standard CNC inserts | |
| Tool Shank Type | Double-ended turning tools | One tool for both external and internal beveling |
| Main Unit Type | Integrally cast structure | |
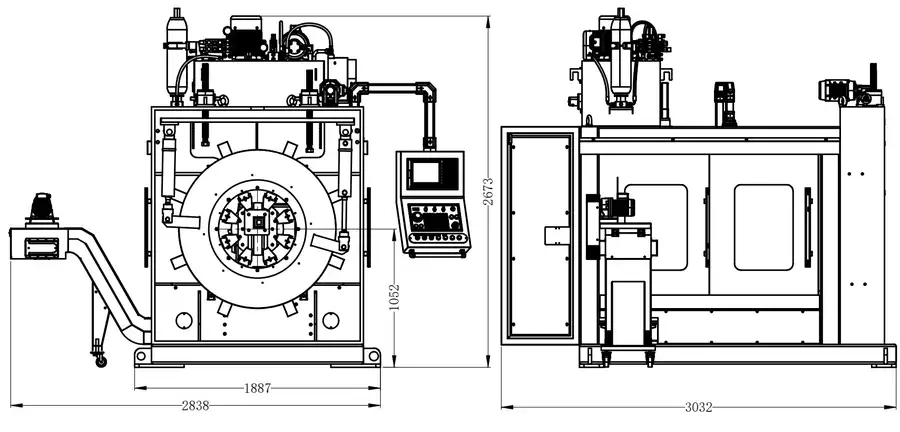
| Overall Dimensions | ||
| Machine Weight |
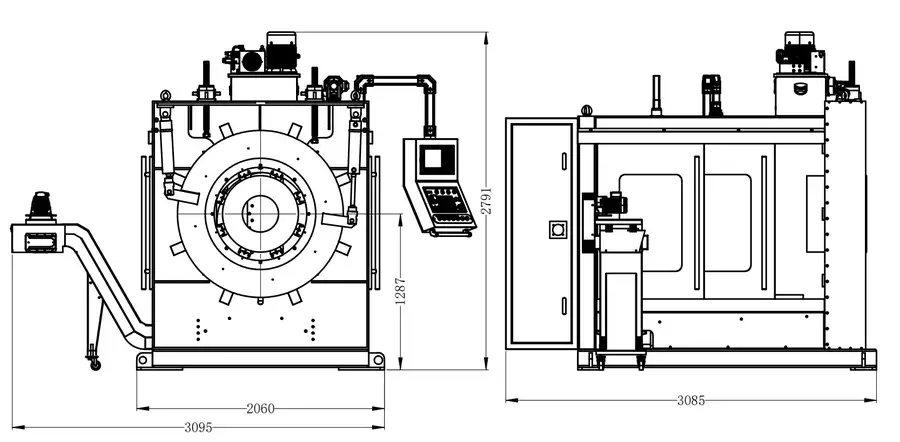
DJ-400 Overall Dimension Drawing (Machining Range: Φ30 – Φ457)
SDJ-600 Main Technical Parameters (Machining Range: Φ80 – Φ630)
| Number | Parameter | Remarks |
| Machining Range | Φ80- Φ 630 | |
| Machinable Wall Thickness | 3-120mm | |
| Bevel Profiles | V, Double V, U, UV, I and other bevel profiles | Custom additional bevel profiles available |
| Clamping Method | Hydraulic multi-jaw clamping | 8-jaw synchronous clamping |
| Control System | Yida, Taiwan | Other control systems optional |
| Suitable Workpiece Materials | Carbon steel, alloy steel, stainless steel, low-temperature steel, etc. | |
| Main Motor Power | 7.5KW | |
| Feeding Speed | Servo control | Adjustable |
| X-axis Servo Motor Power | 2.3KW | |
| Y-axis Servo Motor Power | 2.3KW | |
| Main Unit Guarding Type | Full frame guarding | |
| Chip Removal Type | Rear slat-chain chip removal system | Standard |
| Hydraulic Motor Power | 2.2/ 5 | Optional |
| Vertical & Horizontal Axis Locking Method | Manual / Automatic | Optional |
| Screen Size | 15-inch, 19-inch | Optional |
| Main Unit Lighting | Available | RED lighting |
| X-axis Repeat Positioning Accuracy | ±0.1 | |
| Y-axis Repeat Positioning Accuracy | ±0.1 | |
| Main Motor Transmission Type | Heavy-duty V-belt | |
| Boring Depth | ≤150mm | Standard tool shank: 100 |
| Spindle & Cutter Head Speed | 20–200 rpm | Stepless speed regulation, spindle VFD speed control |
| Tool Type | Standard CNC inserts | |
| Tool Shank Type | Double-ended turning tools | One tool for both external and internal beveling |
| Main Unit Type | Integrally cast structure | |
| Overall Dimensions | ||
| Machine Weight |
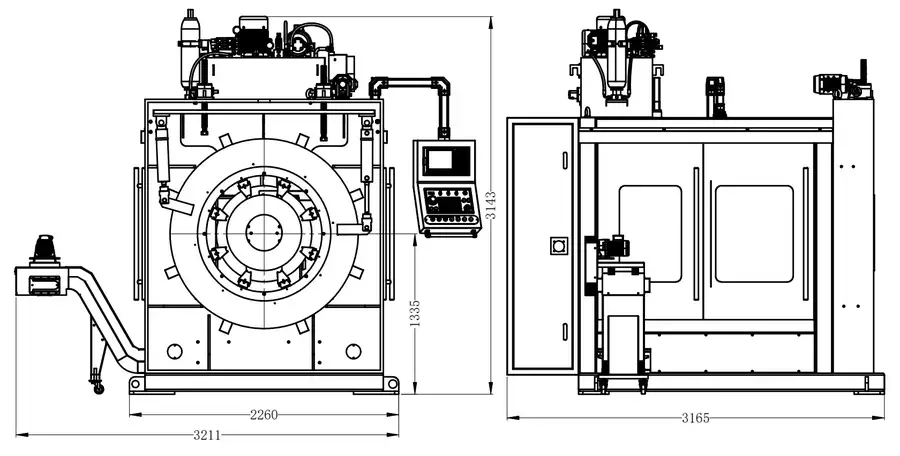
DJ-600 Overall Dimension Drawing (Machining Range: Φ80 – Φ630)
SDJ-800 Main Technical Parameters (Machining Range: Φ200 – Φ830)
| Number | Parameter | Remarks |
| Machining Range | Φ200- Φ 830 | |
| Machinable Wall Thickness | 3-150mm | |
| Bevel Profiles | V, Double V, U, UV, I and other bevel profiles | Custom additional bevel profiles available |
| Clamping Method | Hydraulic multi-jaw clamping | 8-jaw synchronous clamping |
| Control System | Yida, Taiwan | Other control systems optional |
| Suitable Workpiece Materials | Carbon steel, alloy steel, stainless steel, low-temperature steel, etc. | |
| Main Motor Power | 7.5KW | |
| Feeding Speed | Servo control | Adjustable |
| X-axis Servo Motor Power | 2.3KW | |
| Y-axis Servo Motor Power | 2.3KW | |
| Main Unit Guarding Type | Full frame guarding | |
| Chip Removal Type | Rear slat-chain chip removal system | Standard |
| Hydraulic Motor Power | 2.2/ 5 | Optional |
| Vertical & Horizontal Axis Locking Method | Manual / Automatic | Optional |
| Screen Size | 15-inch, 19-inch | Optional |
| Main Unit Lighting | Available | RED lighting |
| X-axis Repeat Positioning Accuracy | ±0.1 | |
| Y-axis Repeat Positioning Accuracy | ±0.1 | |
| Main Motor Transmission Type | Heavy-duty V-belt | |
| Boring Depth | ≤150mm | Standard tool shank: 100 |
| Spindle & Cutter Head Speed | 20–200 rpm | Stepless speed regulation, spindle VFD speed control |
| Tool Type | Standard CNC inserts | |
| Tool Shank Type | Double-ended turning tools | One tool for both external and internal beveling |
| Main Unit Type | Integrally cast structure | |
| Overall Dimensions | ||
| Machine Weight |
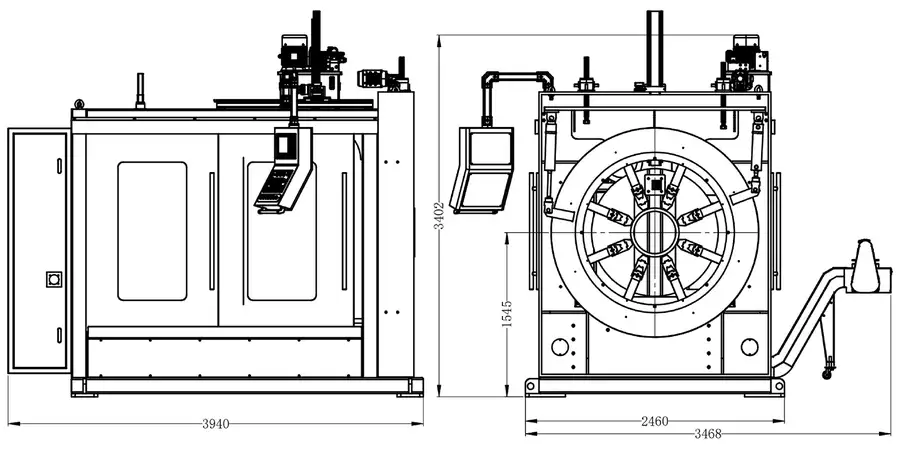
DJ-800 Overall Dimension Drawing (Machining Range: Φ200 – Φ830)
SDJ-1200 Main Technical Parameters (Machining Range: Φ300 – Φ1200)
| Number | Parameter | Remarks |
| Machining Range | Φ300- Φ 1200 | |
| Machinable Wall Thickness | 3-200mm | |
| Bevel Profiles | V, Double V, U, UV, I and other bevel profiles | Custom additional bevel profiles available |
| Clamping Method | Hydraulic multi-jaw clamping | 8-jaw synchronous clamping |
| Control System | Yida, Taiwan | Other control systems optional |
| Suitable Workpiece Materials | Carbon steel, alloy steel, stainless steel, low-temperature steel, etc. | |
| Main Motor Power | 18.5KW | |
| Feeding Speed | Servo control | Adjustable |
| X-axis Servo Motor Power | 2.3KW | |
| Y-axis Servo Motor Power | 2.3KW | |
| Main Unit Guarding Type | Full frame guarding | |
| Chip Removal Type | Rear slat-chain chip removal system | Standard |
| Hydraulic Motor Power | 2.2/ 5 | Optional |
| Vertical & Horizontal Axis Locking Method | Manual / Automatic | Optional |
| Screen Size | 15-inch, 19-inch | Optional |
| Main Unit Lighting | Available | RED lighting |
| X-axis Repeat Positioning Accuracy | ±0.1 | |
| Y-axis Repeat Positioning Accuracy | ±0.1 | |
| Main Motor Transmission Type | Heavy-duty V-belt | |
| Boring Depth | ≤150mm | Standard tool shank: 100 |
| Spindle & Cutter Head Speed | 20–200 rpm | Stepless speed regulation, spindle VFD speed control |
| Tool Type | Standard CNC inserts | |
| Tool Shank Type | Double-ended turning tools | One tool for both external and internal beveling |
| Main Unit Type | Integrally cast structure | |
| Overall Dimensions | ||
| Machine Weight |
DJ-1200 Overall Dimension Drawing (Machining Range: Φ300 – Φ1200)
SDJ-1500 Main Technical Parameters (Machining Range: Φ500 – Φ1500)
| Number | Parameter | Remarks |
| Machining Range | Φ500- Φ 1500 | |
| Machinable Wall Thickness | 3-200mm | |
| Bevel Profiles | V, Double V, U, UV, I and other bevel profiles | Custom additional bevel profiles available |
| Clamping Method | Hydraulic multi-jaw clamping | 8-jaw synchronous clamping |
| Control System | Yida, Taiwan | Other control systems optional |
| Suitable Workpiece Materials | Carbon steel, alloy steel, stainless steel, low-temperature steel, etc. | |
| Main Motor Power | 4KW | |
| Feeding Speed | Servo control | Adjustable |
| X-axis Servo Motor Power | 2.3KW | |
| Y-axis Servo Motor Power | 2.3KW | |
| Main Unit Guarding Type | Full frame guarding | |
| Chip Removal Type | Rear slat-chain chip removal system | Standard |
| Hydraulic Motor Power | 2.2/ 5 | Optional |
| Vertical & Horizontal Axis Locking Method | Manual / Automatic | Optional |
| Screen Size | 15-inch, 19-inch | Optional |
| Main Unit Lighting | Available | RED lighting |
| X-axis Repeat Positioning Accuracy | ±0.1 | |
| Y-axis Repeat Positioning Accuracy | ±0.1 | |
| Main Motor Transmission Type | Heavy-duty V-belt | |
| Boring Depth | ≤150mm | Standard tool shank: 100 |
| Spindle & Cutter Head Speed | 20–200 rpm | Stepless speed regulation, spindle VFD speed control |
| Tool Type | Standard CNC inserts | |
| Tool Shank Type | Double-ended turning tools | One tool for both external and internal beveling |
| Main Unit Type | Integrally cast structure | |
| Overall Dimensions | ||
| Machine Weight |
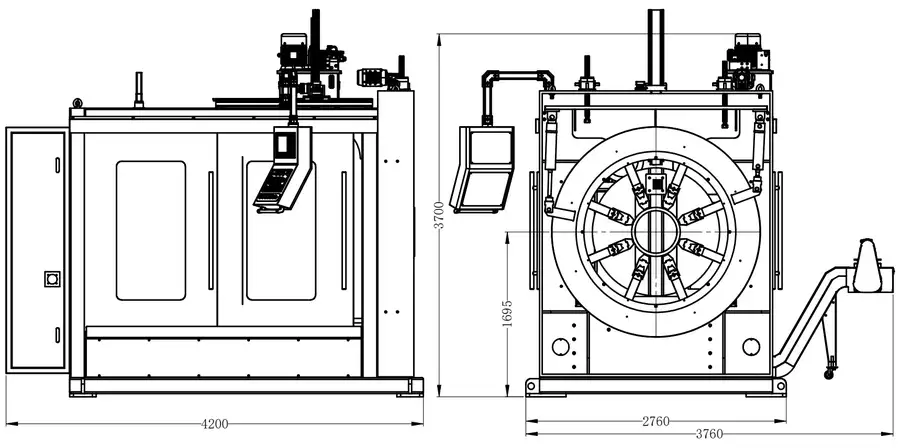
DJ-1200 Overall Dimension Drawing (Machining Range: Φ500 – Φ1500)
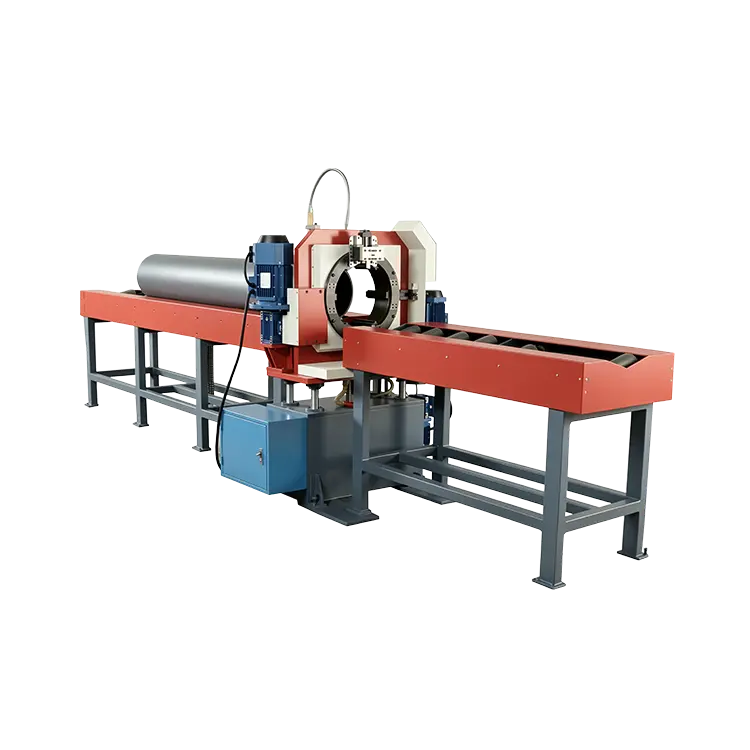
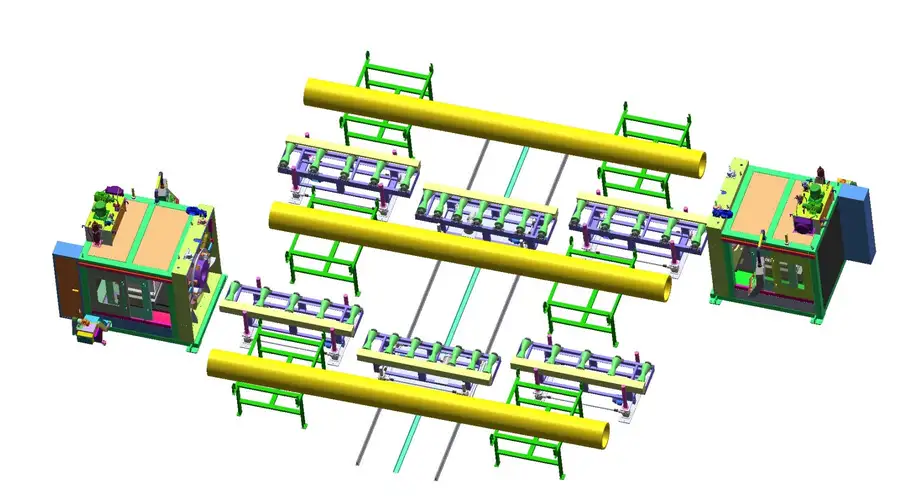
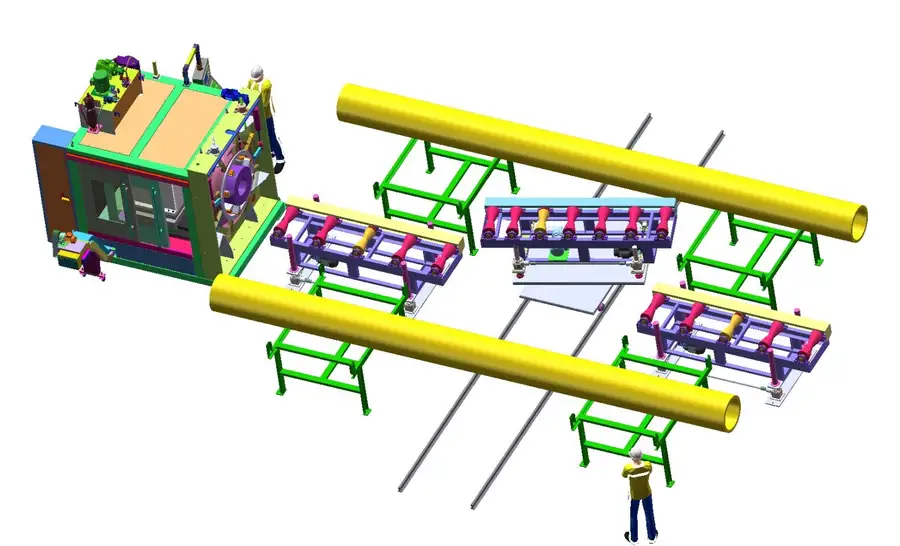
The CNC beveling machine pipe supports multiple layout schemes for streamlined beveling of various pipe diameters. Flexible configurations optimize workflows and improve on-site adaptability and processing capacity.
Roller Material: Carbon steel with high-strength polyurethane coating, V-shaped rollers
Line Length: 6–12 m (customizable length)
Conveying Method: Electric conveying
Conveying Speed: 2–20 m/min
Speed Regulation: VFD stepless speed control
Control System: Wireless remote control
Lifting System: 4–6 electric synchronised lifters, electrically adjusting the pipe center height to accommodate beveling of pipes with different diameters
Traversing Trolley: Cross travel movement, working with racks for streamlined production
Roller Material: Carbon steel with high-strength polyurethane coating, V-shaped rollers
Line Length: 6–12 m (customizable length)
Conveying Method: Electric conveying
Conveying Speed: 2–20 m/min
Speed Regulation: VFD stepless speed control
Control System: Wireless remote control
Lifting System: 4–6 electric synchronized lifters. Electrically adjust pipe center height to suit pipe beveling for different diameters
Automatic Pipe Turning: Enables beveling on both pipe ends
Roller Material: Carbon steel with high-strength polyurethane coating, V-shaped rollers
Line Length: 6–12 m (customizable)
Conveying Method: Electric conveying
Conveying Speed: 2–20 m/min
Speed Regulation: VFD stepless speed control
Control System: Wireless remote control
Lifting System: 4–6 electrically synchronized lifters. It adjusts the pipe center height electrically to adapt to beveling work of pipes with different diameters.
Roller Material: Carbon steel with high-strength polyurethane coating, V-shaped rollers
Line Length: 3 m (customizable, excluding the lower rails)
Conveying Method: Electric conveying
Conveying Speed: 2–20 m/min
Speed Regulation: VFD stepless speed control
Control System: Wireless remote control
Lifting System: 4–6 electrically synchronized lifters. Electric adjustment of pipe center height to accommodate beveling of pipes with different diameters
Automatic Pipe Turning: Supports beveling on both pipe ends
Manually adjust bracket height to align with the machine center
Manually move forward and backward to adjust the support position of steel pipes
A: The frame of the CNC beveling machine pipe is made of thickened material with precision welding, featuring a stable structure and strong impact resistance. Its stainless steel base delivers excellent corrosion and wear resistance, superior protection and long service life.
A: The main body adopts an integral casting process for high machining accuracy and strong structural rigidity. It is equipped with an 8-jaw clamping structure, which provides large contact area and firm clamping to effectively prevent deformation of thin-walled pipes during machining.
A: It adopts rear motor drive and eliminates the traditional front motor plus slip ring structure to reduce failure rates, ensure stable transmission and cut downtime for maintenance.
A: The automatic dual-link centering design enables fast and easy alignment. The independent rear slag removal structure will not affect machining accuracy and allows easier cleaning and maintenance.
Address
Banshang Dalongsi Industrial Zone, Liujia Town, Wujin District, Changzhou City, Jiangsu Province, China
Tel